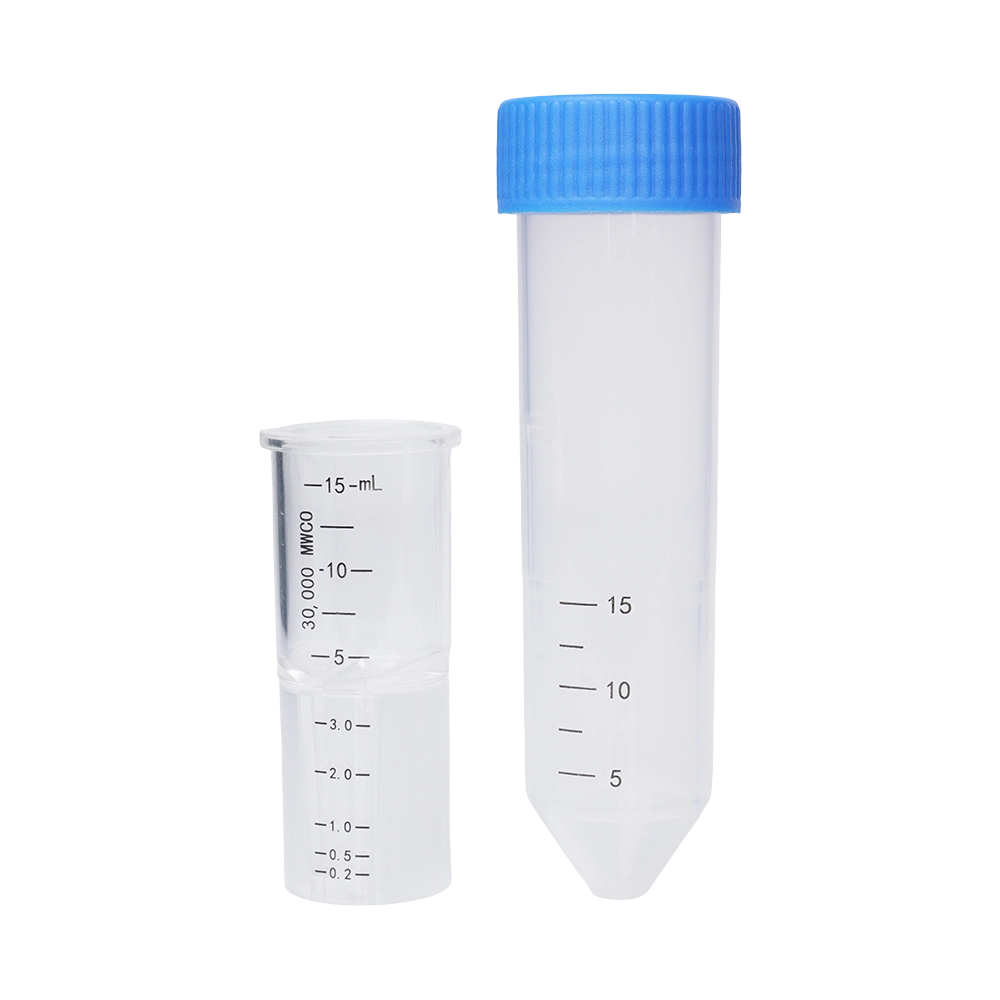
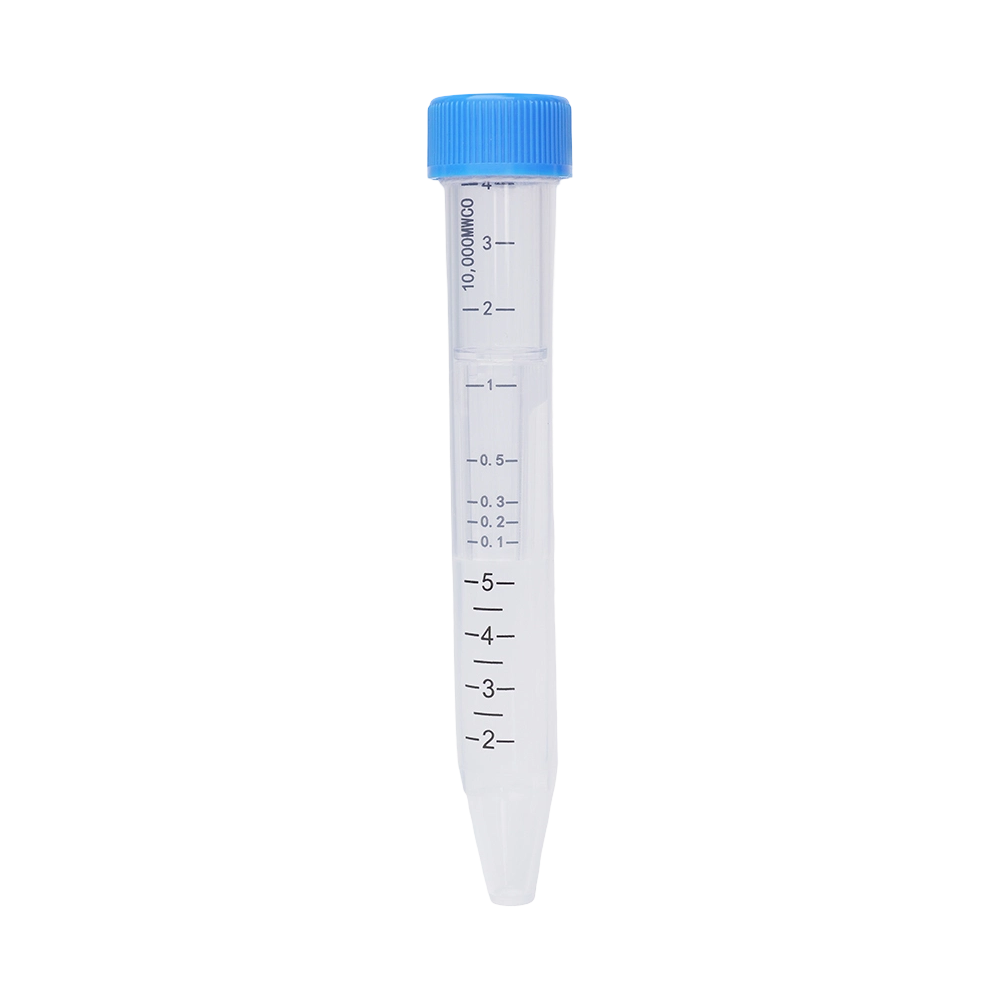
Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube

Home / Products / Laboratory Consumables / Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube

Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube

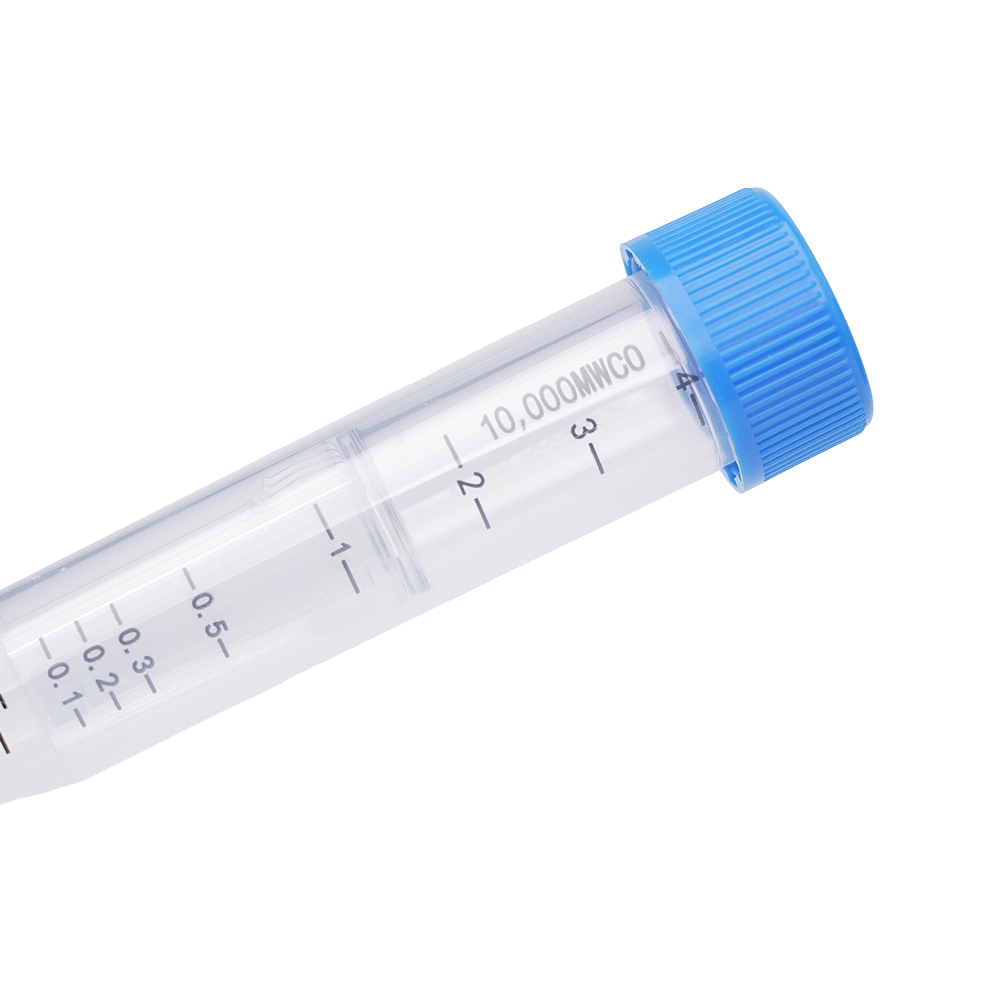
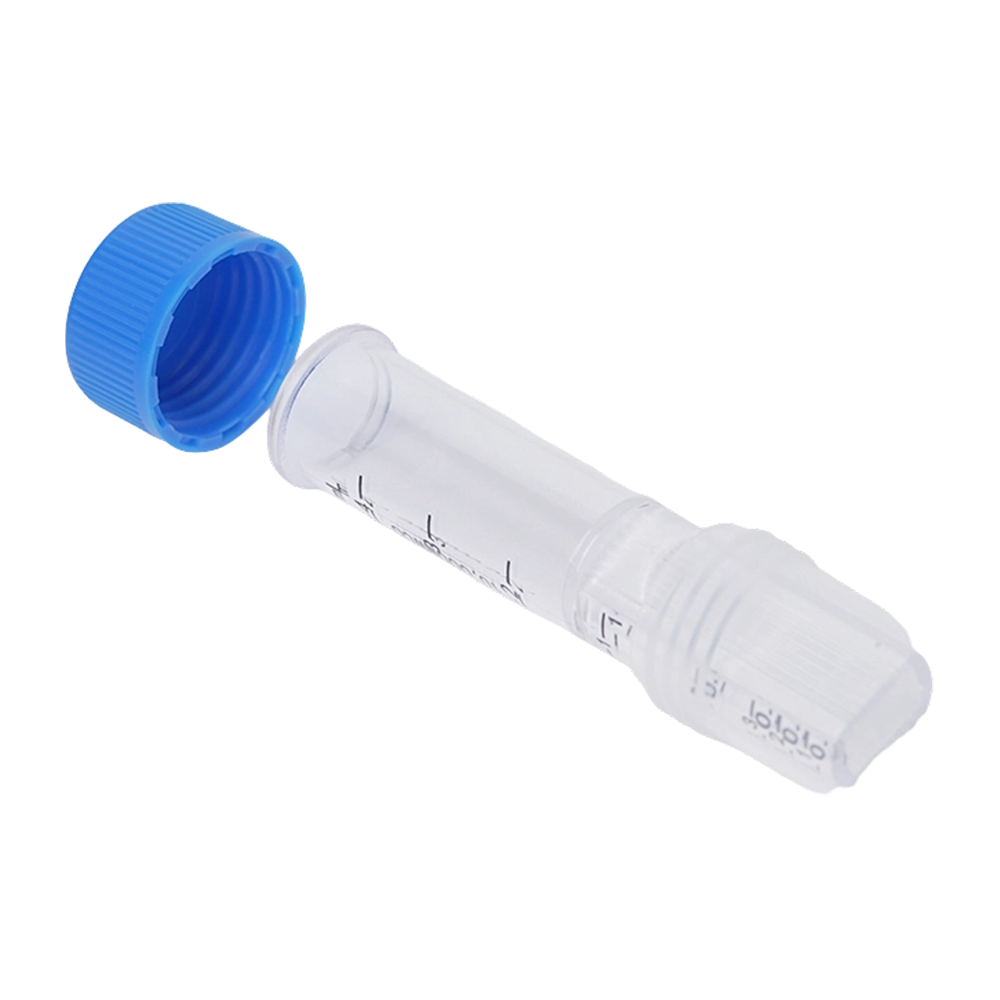
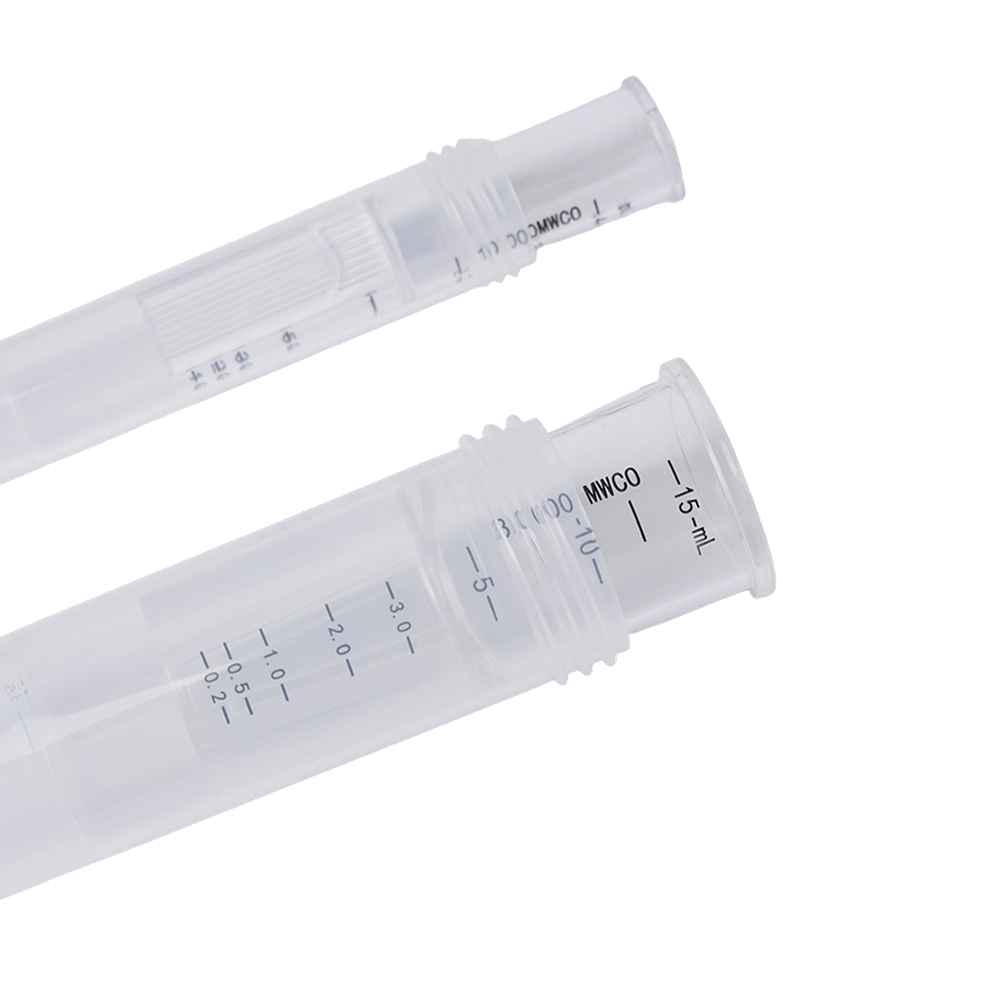
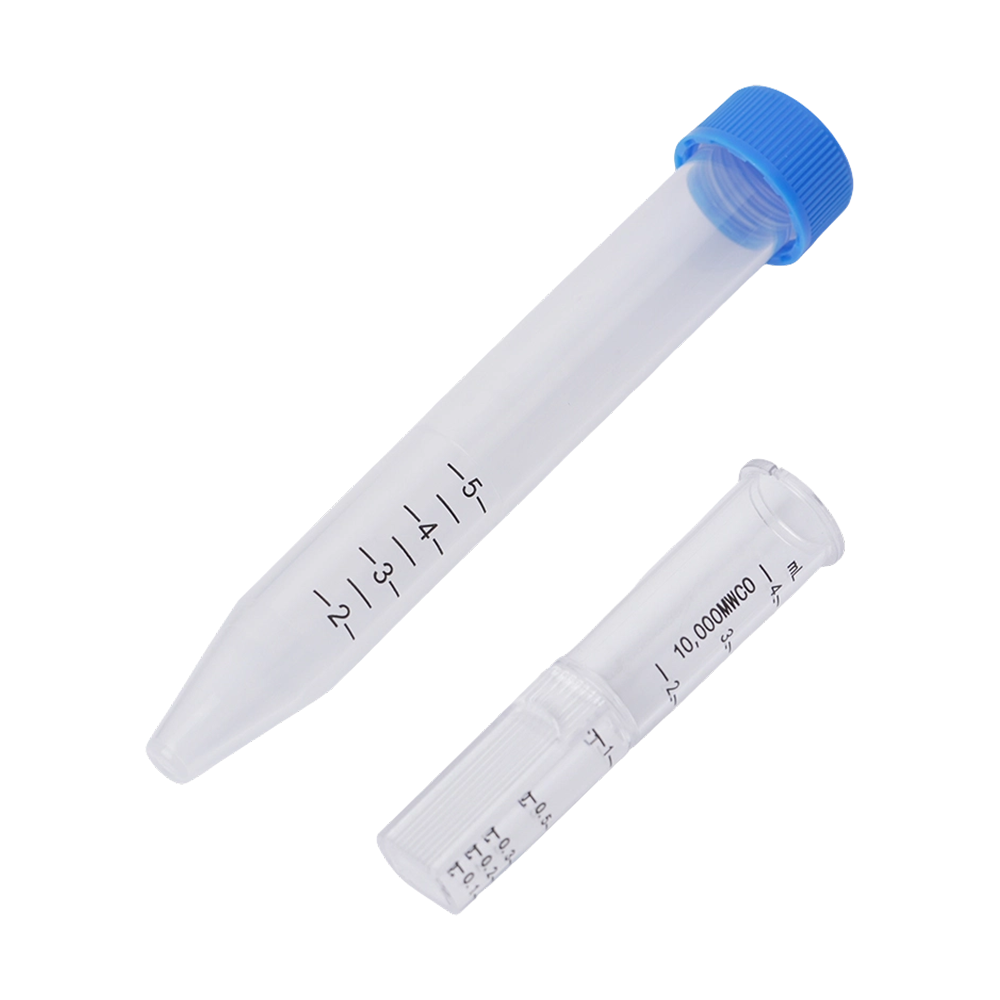
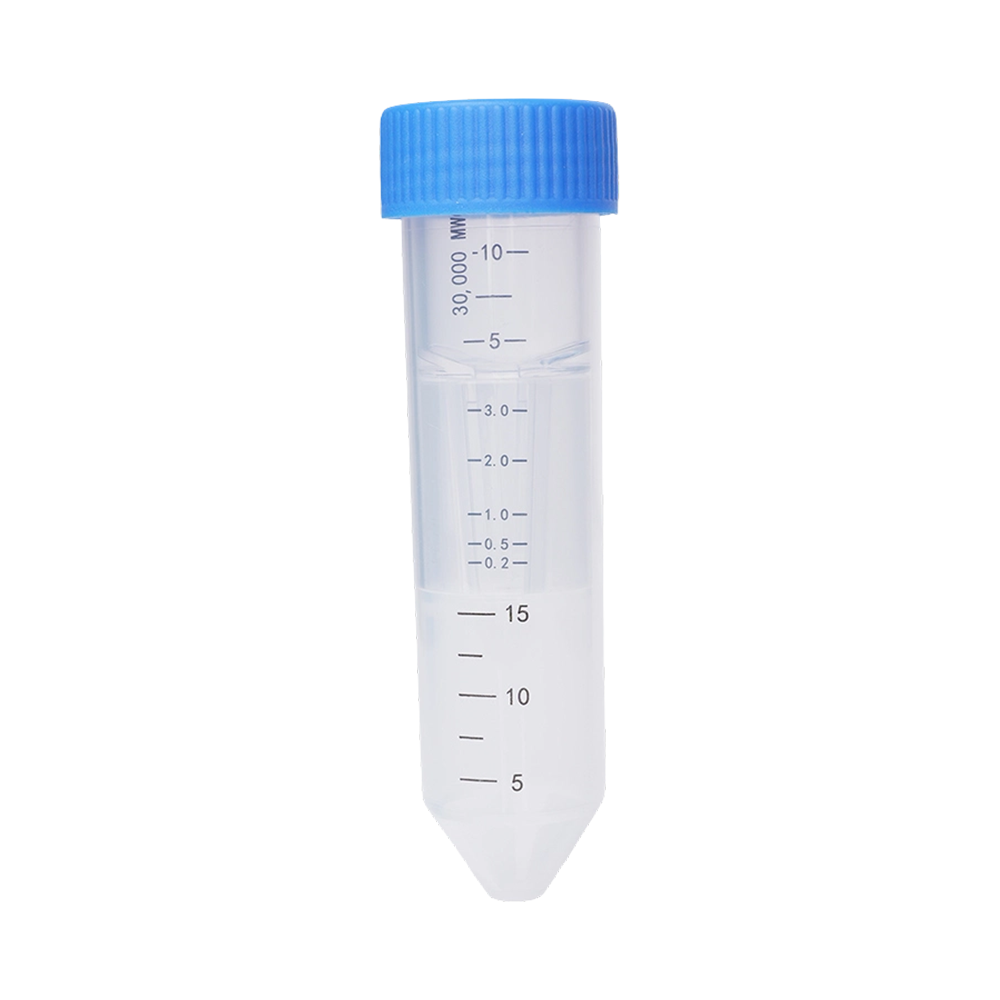
High retention accuracy, low protein adsorption, high recovery rate >90%;Double-sided vertical membrane design, prevent membrane clogging, ultra-low retention volume, high centrifugal efficiency;Excellent biocompatibility and safety, minimal extract, USP87 certified;The anti-drying and locking design can avoid the sample damage caused by excessive centrifugation and ensure the stable and reliable experimental results.Multiple membrane options,OEM custom.

  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
  • Qiujing High Centrifugal Efficiency USP87 Certified Reliable Results Ultrafiltration Centrifuge Tube
Product Catalogue 0.5ml 4ml 15ml
Product Catalog Polycarbonate (PC)
Filter Unit Polysulfone (PSU)
Filter Membrane Polypropylene (PP)
Filtrate Tube Polypropylene (PP)
Filtrate Cap & Liner 0.9cm² 3.5cm² 7.2cm²
Effective Filtration Area Length (concentration mode: filters inserted directly into the outer tube):50.3mm length Total length 122mm The total length is 117mm
(reverse centrifugation: filters inserted into the outer tube):46.8mm Diameter: 10.9mm diameter 17mm Diameter 31mm
Centrifuge Filter Dimensions (With Cap) Length: 29.2mm diameter: 9.4mm Length: 675mm diameter: 145mm Length: 75mm diameter: 28mm
Inner Filter Dimensions ≤5 μl ≤20 μl ≤30 μl
Hold‑up Volume 10‑20 μl 50‑100 μl 300 μl
Dead Volume 0‑40℃
Operating Temperature 1‑14
pH Range 14000g Horizontal centrifugation at 4000g Horizontal centrifugation at 4000g
(100KD is at 3000g)
Maximum Centrifugal Force (Ultrafiltration) Fixed‑angle centrifugation at 6000g Fixed‑angle centrifugation at 5000g
(100KD is 3000ml)
Maximum Centrifugal Force (Microfiltration) / 10000g 6000g
Centrifuge Type Suitable for centrifuges with standard 1.5 mL conical tubes Suitable for centrifuges that can handle standard 15 mL conical tubes Suitable for centrifuges that can handle standard 50 mL conical tubes
Sterilization Before use, it can be disinfected and sterilized by passing through a device that filters 70% ethanol.

Contact Us

Your email address will not be published. Required fields are marked *


  • Message *

  • Name

  • Email *

  • Phone

Shanghai Qiujing Biochemical Reagent & Instrument Co., Ltd. is a pioneering enterprise dedicated to the research, development, and production of precision micropipettes. As a trailblazer in this field in China and a forerunner in replacing imported products with domestically manufactured alternatives, the company has been deeply committed to the laboratory instrument sector since its brand was established in 1988. The brand officially completed the registration of its Chinese and English trademarks in 1992. Driven by a persistent pursuit of technological innovation, the company has continuously advanced its production capabilities, mastering advanced manufacturing and testing technologies, overcoming multiple industry technical challenges, and securing a number of technical patents that provide a solid foundation for product quality.

At the same time, the enterprise has established a comprehensive quality management system and has successfully obtained CE and ISO 13485 quality system certifications. Its sales and service network extensively covers the entire country, while its products are also exported to overseas markets, earning recognition from both domestic and international customers.

ABOUT QIUJING

BELIEVE IN OUR STRENGTH

Shanghai Qiujing Biochemical Reagent & Instrument Co., Ltd.
  • Shanghai Qiujing Biochemical Reagent & Instrument Co., Ltd.
    1988Year

    Founded In

  • Shanghai Qiujing Biochemical Reagent & Instrument Co., Ltd.
    35Year

    Industry Experience

  • Shanghai Qiujing Biochemical Reagent & Instrument Co., Ltd.
    3000

    Factory Area

  • Shanghai Qiujing Biochemical Reagent & Instrument Co., Ltd.
    15+

    Core Products

EXPLORE WHAT'S NEW
Keeping you connected with laboratory innovation
  • Growing demand for precision instruments drives laboratory market development
    2026/08/20
    Industry News
    Growing demand for precision instruments drives laboratory market development

    The global laboratory equipment market is experiencing steady growth as research institutions, medical organizations, and industrial enterprises continue to invest in advanced testing solutions. Precision instruments with stable performance and convenient operation have become important tools for improving laboratory efficiency.

    Equipment including pipettes, centrifuges, sample preparation devices, and analytical instruments plays an important role in daily laboratory operations. With increasing requirements for accuracy and repeatability, manufacturers are focusing on material selection, manufacturing processes, and product improvements to enhance overall product quality.

    In addition, customized solutions are becoming an important trend in the industry. Different application fields require specific product configurations, and professional suppliers are providing flexible options to support various laboratory needs.

    By combining technology development, quality management, and customer-oriented services, the laboratory equipment industry continues to provide reliable solutions for global scientific and industrial applications.

  • Laboratory equipment industry embraces smarter and more efficient solutions
    2026/08/20
    Industry News
    Laboratory equipment industry embraces smarter and more efficient solutions

    With the continuous development of scientific research, healthcare, and industrial testing, the demand for efficient and reliable laboratory equipment continues to grow. Modern laboratories are placing greater focus on equipment accuracy, user-friendly operation, and flexible application capabilities.

    Products such as micropipettes, centrifuges, mixers, and other laboratory instruments are being widely applied in biotechnology, medical testing, pharmaceutical research, and educational laboratories. Manufacturers are continuously improving product design, enhancing operational convenience, and optimizing performance to better meet the diverse requirements of different laboratory environments.

    At the same time, digital technologies and intelligent manufacturing processes are bringing new possibilities to laboratory equipment development. Through improved production techniques and quality control systems, suppliers are helping laboratories achieve more efficient workflows and stable testing performance.

    The laboratory equipment industry is expected to continue evolving with greater attention to precision, reliability, and customized solutions, supporting innovation across various scientific fields.


  • Expanding our global market service network and enhancing the international client experience.
    2026/08/20
    Company News
    Expanding our global market service network and enhancing the international client experience.

    In recent years, the company has continuously improved its overseas market service layout, actively cooperating with customers from different regions to provide professional product support and comprehensive services to global users.

    To meet the needs of international customers, the company has established a service process covering pre-sales consultation, solution communication, order follow-up, and after-sales support, helping customers to complete product selection and procurement more efficiently. At the same time, the company continues to improve its supply chain management capabilities, optimizing production arrangements and delivery processes to ensure orders are processed on schedule.

    Through continuous improvement of product quality and service capabilities, the company has gradually established stable international cooperative relationships. In the future, the company will continue to adhere to its professional development direction, providing more overseas customers with convenient and efficient laboratory equipment solutions.

  • Continuously optimize the product R&D system and promote the upgrade of laboratory solutions.
    2026/08/20
    Company News
    Continuously optimize the product R&D system and promote the upgrade of laboratory solutions.

    As global demands for laboratory technology continue to evolve, the company closely monitors industry application trends and continuously improves its product development system and technical service capabilities. Through in-depth analysis of market demands, the company continuously optimizes product performance, user experience, and application scenarios to provide customers with more suitable laboratory equipment solutions.

    During the R&D process, the company emphasizes the combination of technological innovation and quality management. Through a streamlined production process, rigorous quality testing, and professional team collaboration, the company enhances product stability and user experience. Simultaneously, the company actively collects customer feedback and improves products based on the application needs of different fields, providing reliable support for scientific research, medical, educational, and industrial experiments.

    In the future, the company will continue to increase R&D investment, continuously optimize its product structure and service system, and maintain close cooperation with global customers to jointly promote the development of laboratory technology applications.

Laboratory Consumables Industry knowledge